 CedarExSports Global CedarExSports Global
Explore our certified match-grade and high-retention training football lineup. Engineered with weather-resistant thermal bonding, high-density PU covers, and reinforced latex bladders optimized for North American turf and outdoor play.
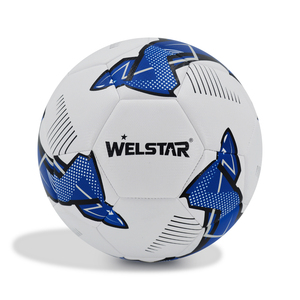
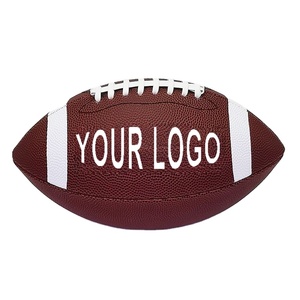
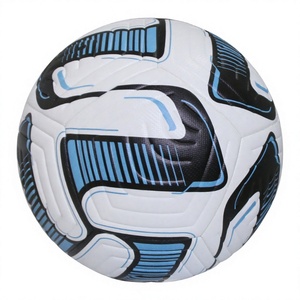
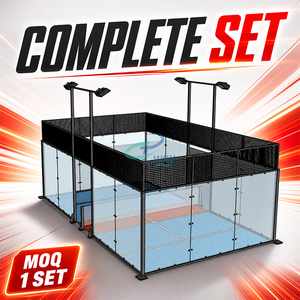
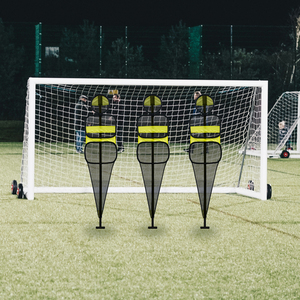
As a leading global OEM/ODM manufacturer headquartered in Sialkot—the world's historic hub for inflatable sports ball production—CedarEx Sports Global provides high-altitude, cold-weather, and high-abrasion training footballs custom-engineered for the Greater Boston metropolitan market and New England athletic leagues. Procurement officers, university athletic directors across Cambridge, Chestnut Hill, and Boston, alongside independent sporting goods distributors, face distinct environmental and performance challenges when acquiring bulk training balls.
The New England soccer ecosystem—ranging from NCAA Division I and III collegiate powerhouses to high-school athletic conferences (MIAA), club networks (NEP, MAPLE, GPS), and urban indoor turf domes—operates under intense seasonal variations. Standard off-the-shelf training footballs frequently fail due to three localized stresses:
Customized equipment manufacturing is not a one-size-fits-all process. We engineer specialized training footballs, rugby balls, and athletic training obstacles tuned specifically for local training environments across Massachusetts:
Designed for intense spring practice regimens at university complexes in Boston, Cambridge, and Waltham. Featuring 32-panel thermo-bonded seamless technology that matches FIFA Quality Pro flight dynamics, permitting varsity players to train with match-identical ball mechanics without depleting game-ball inventories.
Soft-touch micro-textured PU construction (Sizes 3, 4, and 5) ideal for developmental clubs across Greater Boston. Engineered with high-density EVA shock-absorption inner layers to reduce heading impact velocity while retaining lively responsiveness on cold turf facilities.
Purpose-built low-rebound and high-abrasion fusion training footballs tailored for indoor sports arenas, cage soccer setups, and Padbol court facilities across New England. Reinforced panels resist wall impacts and hard surface friction.
The sports equipment sourcing landscape in New England is undergoing significant structural shifts. Importers, brand owners, and institutional buyers in the Boston area are abandoning low-cost, disposable training gear in favor of sustainable, high-longevity OEM solutions. Key commercial trends include:
Market demand for traditional hand-stitched balls in youth match environments is declining by 8.4% annually, while seamless thermo-bonded training footballs are growing at 14.2% CAGR. Buyers prioritize zero water uptake during wet spring games and smooth aerodynamic trajectory.
Boston-based institutional buyers now enforce rigorous chemical safety profiles. All materials produced in our audited facilities meet EU REACH, OEKO-TEX Standard 100, and U.S. CPSIA standards—guaranteeing phthalate-free, non-toxic PVC/PU materials safe for youth players.
To assist Boston procurement teams in evaluating bulk factory quotes, the table below provides technical criteria across our primary production lines:
| Construction Tech | Outer Material | Bladder Type | Water Absorption | Turf Longevity | Recommended Boston Usage |
|---|---|---|---|---|---|
| Thermo-Bonded Seamless | 1.2mm Textured Japanese PU | Taiwan Butyl + Winding | < 0.5% (Impermeable) | 500+ Intense Field Hours | NCAA / Varsity / Pro Academies |
| Dual-Fusion Hybrid | 1.0mm Structured TPU/PU | Synthetic Rubber / Latex | < 2.0% (High Resistance) | 400+ Field Hours | High School & Club Training |
| Reinforced Hand-Stitched | 1.4mm PU / PVC Grain | Stuffed Latex / Butyl | < 4.5% (Standard) | 350+ Field Hours | Grass Pitch Developmental Leagues |
| Machine-Stitched Soft | 0.2mm TPU + EVA Foam | Natural Rubber Bladder | < 8.0% (Basic) | 200+ Field Hours | Youth Promotional & Skill Practice |
CedarEx Sports Global is an established OEM & private-label manufacturer with state-of-the-art production facilities based in Sialkot, Pakistan, complemented by our European trade office in Monterotondo, Italy, and a dedicated logistics network servicing major U.S. East Coast ports including the Port of Boston (Conley Terminal) and Boston Logan Cargo Hub.
Our manufacturing plants operate under WRAP, SEDEX/SMETA, amfori BSCI, and ISO 9001:2015 standards. We strictly guarantee fair wages, zero child labor, safe operating conditions, and complete supply chain transparency.
From full vector logo printing and custom pantone matching to bespoke panel layout designs and barcode retail packaging—we transform your brand concepts into market-ready athletic goods within 10 to 14 days.
We eliminate import complexity for Boston buyers by managing complete end-to-end logistics under Delivered Duty Paid (DDP), FOB, CIF, or CFR Incoterms. Customs clearance, U.S. tariffs, and inland freight directly to your warehouse are handled seamlessly.
To maintain zero defect rates, every batch of training footballs destined for North American importers undergoes rigorous testing before container sealing:
Tensile strength tests on PU sheets, backing foam thickness checks, and bladder pressure retention validation prior to cutting.
Monitoring bonding thermal temperatures, stitch-per-inch density, seam alignment, and carcass symmetry during active production lines.
Automated sphericity calibration, 2,000-cycle drum impact testing, water absorption immersion analysis, and precise rebound measurement.
Carton drop tests, barcode scan validation, container seal checks, and instant release of Certificate of Origin & Bill of Lading.
Everything you need to know about factory direct orders, customization, lead times, and shipping to Massachusetts.
Elevate your athletic brand, university equipment stock, or regional distribution catalog with factory-direct pricing, audited Sialkot craftsmanship, and reliable Boston DDP delivery.