 CedarExSports Global CedarExSports Global
Direct factory manufacturing specifications for professional match balls, training gear, and combat equipment built under audited AQL 2.5 quality control.
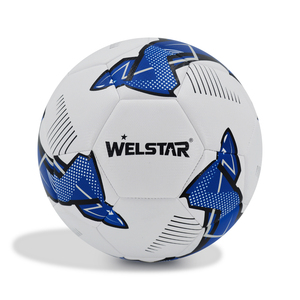
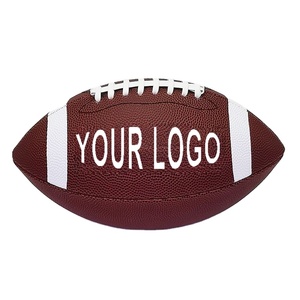
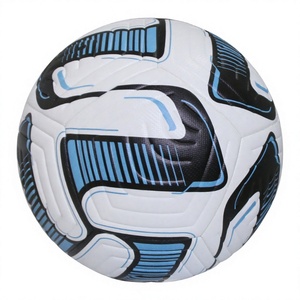
An analytical overview of OEM/ODM operations, modern material science, and strategic sourcing protocols for international sports brands, wholesalers, and governing bodies.
Navigating the global sports equipment market requires a nuanced understanding of manufacturing ecosystems. Sialkot, Pakistan stands as the undisputed heartland of global match ball production, crafting hand-stitched, thermo-bonded, and hybrid inflatable balls for elite world tournaments. By merging centuries-old artisan leathercraft with automated polymer molding, certified manufacturing hubs deliver high-rebound, hydro-repellent match gear optimized for rigorous international competition.
To mitigate international trade friction, top-tier sports equipment exporters operate integrated dual-hub logistical systems. Primary manufacturing, labor compliance audits, and raw material sourcing take place at modern industrial complexes in Pakistan, while administrative, VAT handling, and European Union import clearing are co-managed through strategic European desks (such as our partner desk, Penta Flora SRL in Monterotondo, Italy). This ensures seamless DDP (Delivered Duty Paid) door-to-door delivery.
In modern sports equipment engineering, performance relies heavily on chemical composition and mechanical construction. Professional soccer balls, rugby balls, and combat equipment undergo intense stress during gameplay. High-density Polyurethane (PU) and Thermoplastic Polyurethane (TPU) outer covers have largely superseded legacy PVC in premium tiers, providing superior elasticity, thermal stability, and soft-touch tactile response even under sub-zero pitch conditions.
The transition from traditional 32-panel hand-stitched balls to advanced 20-panel, 14-panel, and seamless 6-panel thermo-bonded match balls represents a major technological leap. Thermo-bonding utilizes high-frequency thermal fusion presses that weld outer panels onto a carcass wrapped in latex or butyl bladders. This process creates an completely water-impermeable barrier, ensuring near-zero water absorption (< 1.5% under FIFA Quality Pro testing guidelines) and uniform aerodynamic drag coefficients across high-velocity trajectories.
Beyond match balls, elite sports equipment suppliers engineer professional boxing and MMA protective equipment, padel rackets, and sublimated team kits. Combat gear production demands strict ergonomic foam molding: multi-layered EVA, latex foam, and high-density gel layers are contoured to distribute impact force, protecting metacarpal bones during high-impact sparring.
In sportswear, eco-friendly sublimation printing with non-toxic, REACH-compliant water-based inks allows infinite custom colorways without compromising fabric breathability or structural GSM integrity. Recycled polyester blends (GRS certified) are increasingly deployed to satisfy corporate sustainability mandates across European and North American retail networks.
To assist institutional buyers, sports brands, and procurement officers, the matrix below outlines core material specifications, minimum order quantities (MOQ), and performance metrics across key equipment lines.
| Equipment Category | Primary Material Build | Construction Type | Standard MOQ | AQL Quality Check Target |
|---|---|---|---|---|
| Match Footballs | 1.2mm - 1.5mm Japanese PU / TPU micro-texture | Thermal-Bonded / Hand-Stitched (32 or 14 Panel) | 100 Pcs | AQL 1.5 / FIFA Quality Standard |
| Training Footballs | 0.8mm - 1.0mm Soft Touch PVC / PU Blend | Machine Stitched / Hybrid Bonding | 100 Pcs | AQL 2.5 Standard Inspection |
| Pro Rugby / American Football | Grained Vulcanized Rubber / Premium PU Leather | Multi-Ply Hand Laminated & Stitched | 100 Pcs | AQL 2.5 Air Retention & Shape Test |
| Combat Equipment (Gloves/Pads) | Genuine Cowhide Leather / Engineered Microfiber PU | Multi-Layer Hand Molded Foam / Reinforced Stitching | 100 Pairs | AQL 2.5 Impact & Weight Tolerance |
| Sublimated Team Jerseys | 140 - 180 GSM Moisture-Wicking Polyester / Spandex | Full Digital Italian Ink Sublimation | 50 Pcs | AQL 2.5 Colorfastness & Seam Pull |
| Carbon Fibre Padel Rackets | 3K / 12K / 18K Carbon Fiber Face + Soft EVA Core | Custom Compression Molded Frame | 50 Pcs | AQL 1.5 Balance & Flex Index |
Understanding macroeconomic shifts, regulatory pressures, and material technological advancements shaping global sports goods supply chains.
Global regulatory bodies like the EU REACH and EPA are tightening restrictions on phthalates, solvent-based adhesives, and virgin plastics. Sourcing trends for 2026–2032 mandate bio-based TPU covers derived from renewable plant oils, recycled PET thread, and water-based bonding glues that reduce volatile organic compound (VOC) emissions during manufacturing by up to 85%.
Modern B2B importers no longer accept blind sourcing. Future-ready exporters provide real-time digital auditing. Inspection photos, video logs, thread pull tests, and spherical rebound statistics are logged at raw material stage, mid-line stitching, and pre-container loading, allowing buyers to verify batch compliance remotely.
Global freight disruptions have made single-point logistics high-risk. Leading suppliers combine competitive Asian/South-Asian production costs with European trade support desks. By routing invoices and customs formalities through EU-domiciled partner entities (e.g., Italy desk), buyers reduce currency exchange volatility and streamline European VAT and import tariff procedures.
Combining century-old craftsmanship, internationally audited facilities, and rigid multi-stage quality assurance.
Our partner manufacturing complexes operate strictly within verified social and environmental frameworks: WRAP, SEDEX / SMETA, amfori BSCI, ISO 9001:2015, ISO 14001, OEKO-TEX Standard 100, and REACH compliance. No child labor, guaranteed fair living wages, and documented worker safety programs.
Every single order undergoes rigorous raw material verification, in-line stitching audits, final AQL 2.5 random sampling (circumference, sphericity, rebound, air-retention, and seam strength testing), and pre-shipment container loading supervision with comprehensive photo/video reporting.
From Karachi export shipping hubs to European partner facilities (Penta Flora SRL, Monterotondo, Italy), we handle Incoterms including FOB, CFR, CIF, and full DDP door-to-door freight options across sea, air, and international rail networks.
From initial artwork, logo sublimation, debossing, panel custom molds, to custom GSM fabric blends and retail packaging with your barcodes—we turn complex technical tech packs into market-ready commercial inventory with pre-production samples delivered in 7-12 days.
Direct answers to crucial buyer questions regarding order minimums, timelines, quality control, custom private-label branding, and customs documentation.
Our MOQs are structured by product family to balance production efficiency and accessibility for growing brands:
Sampling and bulk turnaround times are strictly documented before order confirmation:
We accommodate flexible international trade terms including FOB (Karachi), CFR, CIF, and fully Delivered Duty Paid (DDP). Our Karachi export desk issues complete commercial paperwork (Invoice, Packing List, Bill of Lading, Certificate of Origin, GSP+ documents). For European Union clients, our partner office Penta Flora SRL in Monterotondo (RM), Italy assists with local customs clearances, VAT compliance, and streamlined European bank settlements.
Yes. We specialize in comprehensive OEM/ODM manufacturing. You can provide your exact tech pack specifications—including panel layout, bladder compound (latex vs. butyl), leather density, foam mold layering, carbon racket layup, fabric GSM, and color codes. Branding methods include dye sublimation, screen printing, high-density embroidery, debossing/embossing, custom woven labels, printed hang tags, and retail-ready packaging with custom barcodes.
Quality protection is integrated into every manufacturing stage under our 4-point protocol: (1) Raw Material Verification, (2) In-Line Stitching Audit, (3) Final AQL 2.5 Random Inspection (testing weight, circumference, sphericity, rebound, and seam strength), and (4) Container Loading Verification. Photo and video reports are provided prior to dispatch. If a verified defect rate exceeds agreed AQL thresholds, replacement units are prioritized and produced in the next dispatch window.
Our partner manufacturing complexes hold accredited certifications including WRAP, SEDEX / SMETA, amfori BSCI, ISO 9001:2015, ISO 14001, OEKO-TEX Standard 100, GRS/RCS (Recycled Claim Standard), and REACH compliance, with ball production aligned to FIFA Quality Programme laboratory standards. Audit documents are available upon request for verified corporate buyers.
Connect with our engineering and export team. Receive costed FOB/CIF/DDP proposals, technical sample approvals, and guaranteed production timelines within 24 hours.