 CedarExSports Global CedarExSports Global
An authoritative analysis on polymer molecular binding, technical fabric performance, and modern supply chain optimization for global sports apparel brands.
In the high-performance sportswear sector, dye-sublimation printing has evolved from a simple customization method into a sophisticated chemical engineering process. Unlike traditional screen printing or direct-to-garment (DTG) applications—which deposit a surface layer of plastisol ink that blocks fabric breathability and suffers from cracking—full sublimation creates a molecular bond with synthetic polymer fibers.
Under high heat (190°C to 210°C) and calibrated pneumatic pressure, solid disperse dyes convert directly into gas without passing through a liquid state. This gaseous dye penetrates the opened cross-section of polyester filaments. Upon cooling, the polymer chains close, trapping the pigment inside the fiber core. The result is zero added weight, 100% unimpeded airflow, and absolute colorfastness under rigorous athletic conditions.
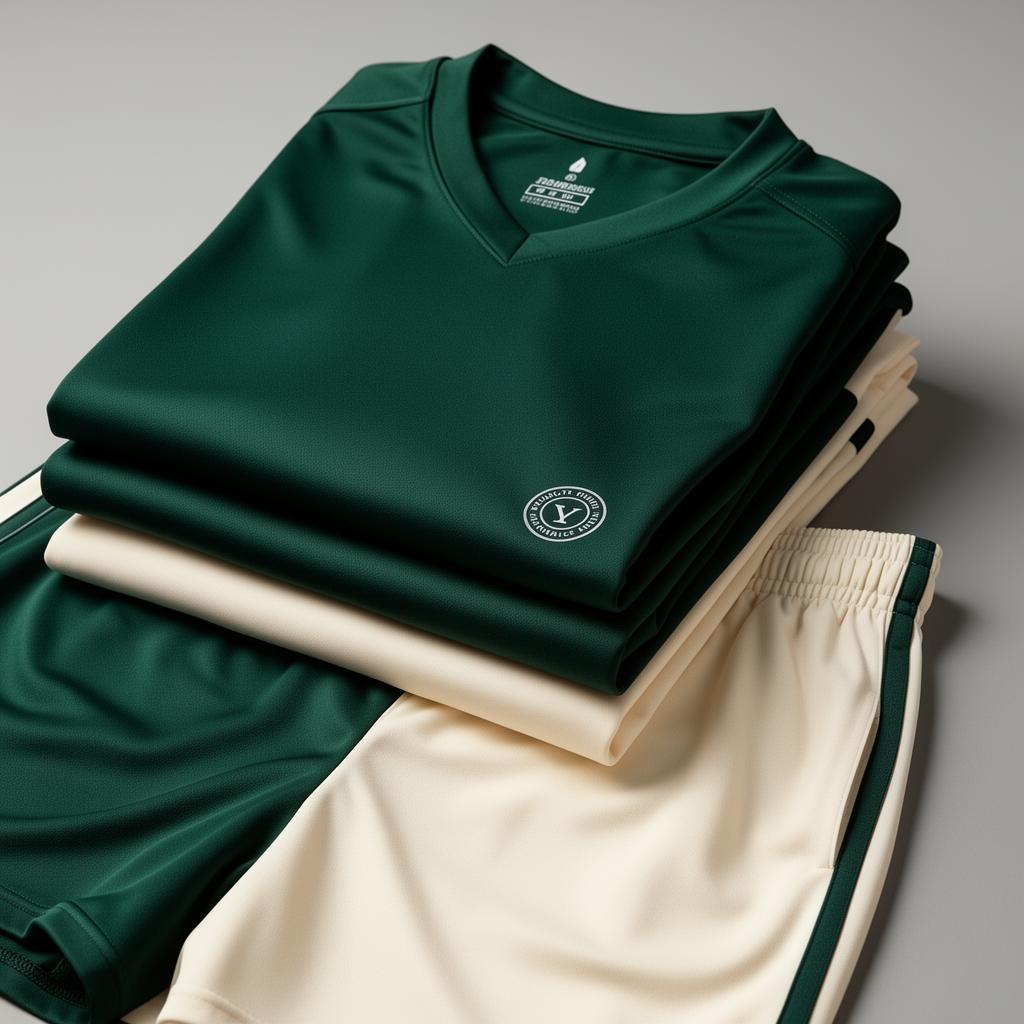
Explore our audited production capabilities spanning sublimated teamwear, professional training balls, and specialized sports gear engineered in Sialkot and distributed globally.
Key structural shifts shaping global OEM sourcing: sustainability metrics, smart thermoregulation, and agile low-MOQ supply chains.
Global brand compliance mandates post-consumer recycled polyester (rPET) derived from ocean plastics. Modern OEM factories are transitioning to Global Recycled Standard (GRS) certified 100% recycled yarns, maintaining identical tensile strength and ink absorption characteristics as virgin polyester while reducing carbon footprints by up to 45%.
Simple wicking finishes are being replaced by permanent hydrophilic micro-grooves integrated directly during yarn extrusion. Advanced silver-ion and peppermint-oil bio-based treatments provide anti-odor properties that withstand 50+ industrial wash cycles, meeting strict EU REACH compliance standards.
B2B procurement leaders require flexible re-order capabilities. The dual-hub model—combining cost-effective bulk OEM manufacturing in Sialkot, Pakistan, with European customs clearing and trade coordination (e.g., via Italy)—reduces lead times while supporting low 50-piece reorder minimums.
| Fabric Material Grade | GSM Range | Primary Athletic Application | Key Performance Attribute | Sublimation Temperature |
|---|---|---|---|---|
| Micro Interlock Polyester | 140 – 160 GSM | Soccer, Running, Esports Jerseys | Ultra-lightweight, rapid evaporative cooling | 200°C (35 seconds) |
| Bird-Eye Poly Mesh | 160 – 180 GSM | Basketball, Field Hockey, Volleyball | High ventilation airflow, tear-resistant mesh | 205°C (30 seconds) |
| Heavyweight Lycra / Spandex Blend | 220 – 260 GSM | Rugby, Compression Wear, MMA Shorts | 4-way elastic stretch, reinforced seam load | 195°C (40 seconds) |
| Recycled rPET Micro-Piqué | 150 – 170 GSM | Eco-Friendly Team Kits, Polos | GRS Certified, zero virgin plastic content | 198°C (38 seconds) |
Direct technical answers for commercial buyers, inventory managers, and OEM private-label brand directors.
Combining Sialkot's historical manufacturing heritage with modern European operational compliance.
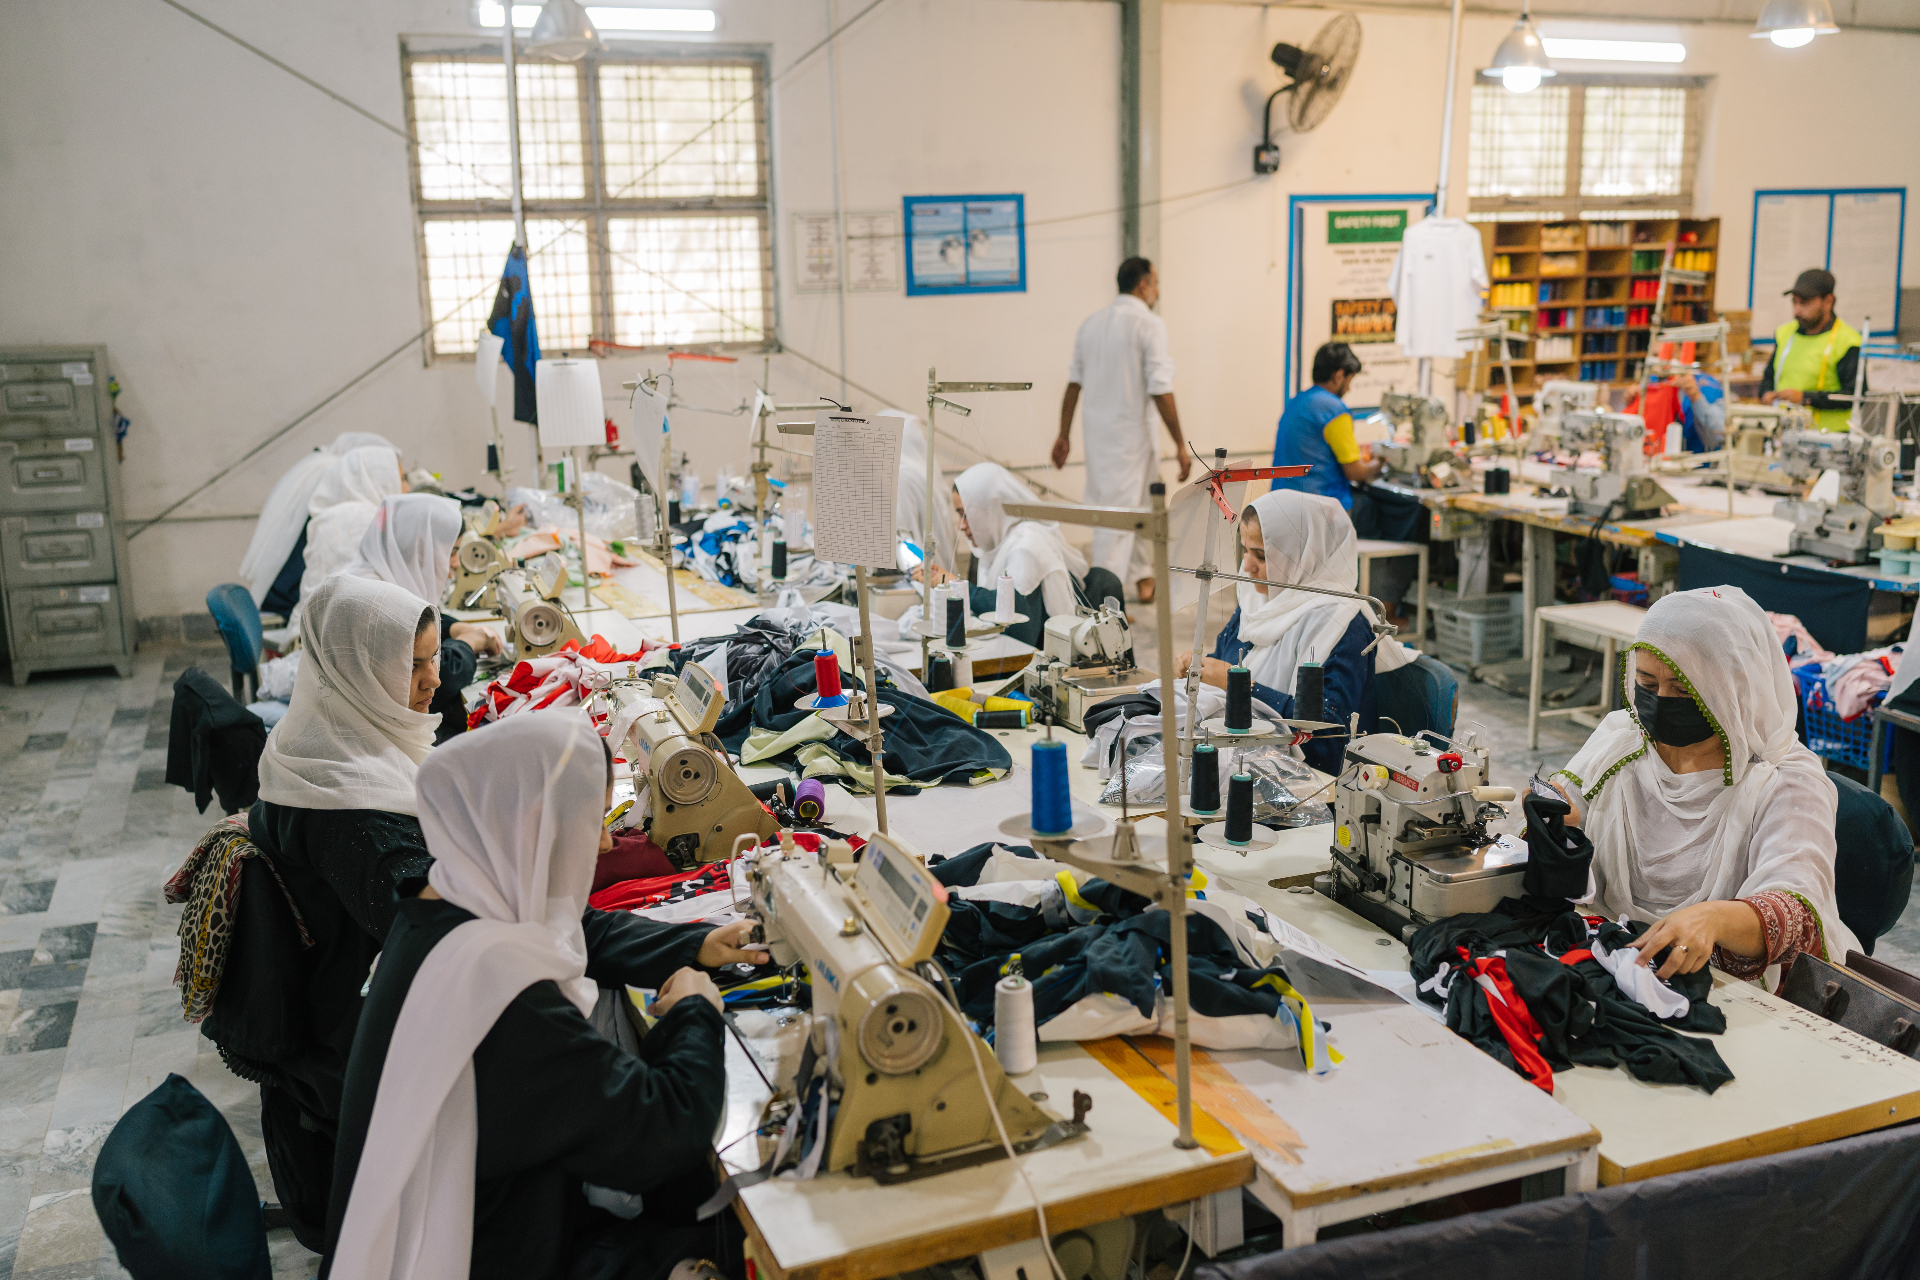
CedarEx Sports Global operates in partnership with fully audited manufacturing facilities in Sialkot, Pakistan. Our production lines comply with global workplace standards, ensuring zero child labor, fair living wages, safe ergonomic environments, and stringent waste-water treatment controls.
Request detailed factory pricing, physical material swatches, and technical production timelines from our global desk today.
Inquire Now