 CedarExSports Global CedarExSports Global
Explore our primary export series manufactured under audited ISO 9001:2015 and AQL 2.5 quality control standards. Custom sizes, technical materials, and private branding tailored for international sporting equipment distributors.
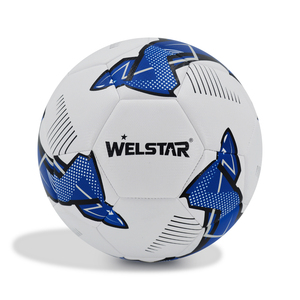
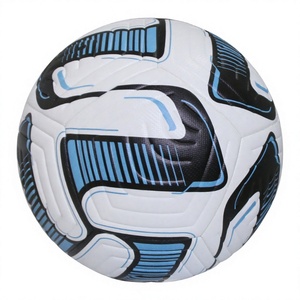
In the global sporting goods sector, selecting an audited, specialized OEM (Original Equipment Manufacturer) is the single most critical factor for brand integrity, tactile performance, and long-term supply chain resilience. As elite basketball leagues, corporate sports distributors, and private-label athletic brands scale their global footprints, the technical parameters of basketball manufacturing—ranging from composite polyurethane (PU) polymer density and nylon-filament winding tension to carcass vulcanization and dynamic moisture absorption—have become key differentiators.
Modern high-performance basketballs are engineered through a complex multi-layered carcass assembly. At CedarEx Sports Global, our OEM manufacturing facilities in Sialkot, Pakistan integrate century-old leather craftsmanship with state-of-the-art thermal lamination and carcass vulcanization lines.
The inner core features a high-percentage butyl bladder, which provides zero-leakage air retention across fluctuating atmospheric pressures. This bladder is encapsulated within thousands of meters of high-tenacity nylon thread windings, ensuring structural roundness, precise rebound response, and permanent shape retention under high-impact game conditions.
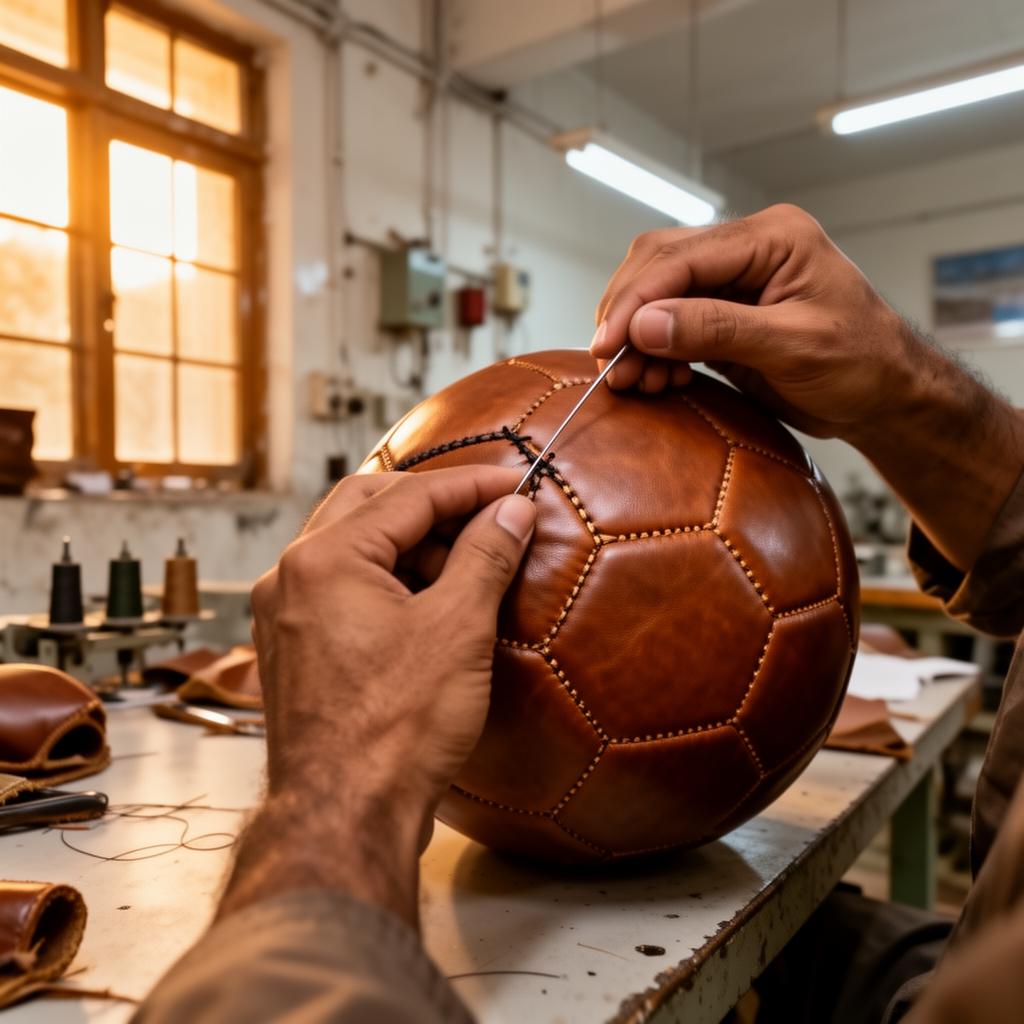
From professional indoor match balls to heavy-duty outdoor rubber basketballs, soccer match balls, and combat equipment, OEM performance is governed by strict chemical and mechanical standards.
Engineered with a micro-porous structure that absorbs surface moisture and sweat during intense play, providing maximum tackiness and non-slip grip. Ideal for official tournament basketballs and premium indoor training gear.
Eliminating traditional seam stress points, thermal bonding fuses carcass panels under calibrated pressure and heat. This process ensures 100% spherical uniformity, zero water absorption, and hyper-predictable flight trajectories.
Full private-label customisation allows clients to engineer exclusive channel layouts, debossed logo textures, foil hot-stamping, and custom Pantone-matched outer panels for worldwide retail distribution.
The global sports equipment manufacturing industry is undergoing structural transformations driven by sustainability mandates, supply chain decentralization, and digital quality auditing. Sourcing directors and OEM brand managers must adapt to four critical procurement trends shaping the 2026–2030 landscape:
International athletic brands are enforcing Global Recycled Standard (GRS) compliance across synthetic leather, backing foams, and packaging. Eco-friendly bio-based PUs and solvent-free waterborne adhesives are replacing traditional PVC.
To mitigate shipping volatility, leading OEM manufacturers deploy hybrid logistics: combining primary mass manufacturing in Pakistan with European trade desks for rapid duty-paid (DDP) warehousing, clearance, and VAT settlement.
Paper inspection certificates are being superseded by transparent photo/video inspection logs at four critical checkpoints: raw material verification, in-line stitching audits, spherical compression tests, and pre-loading checks.
The rise of niche sportswear brands requires flexible OEM lines capable of delivering low MOQs (from 50–100 pieces per design) without imposing prohibitive tooling costs for custom artwork, screen printing, or embroidery.
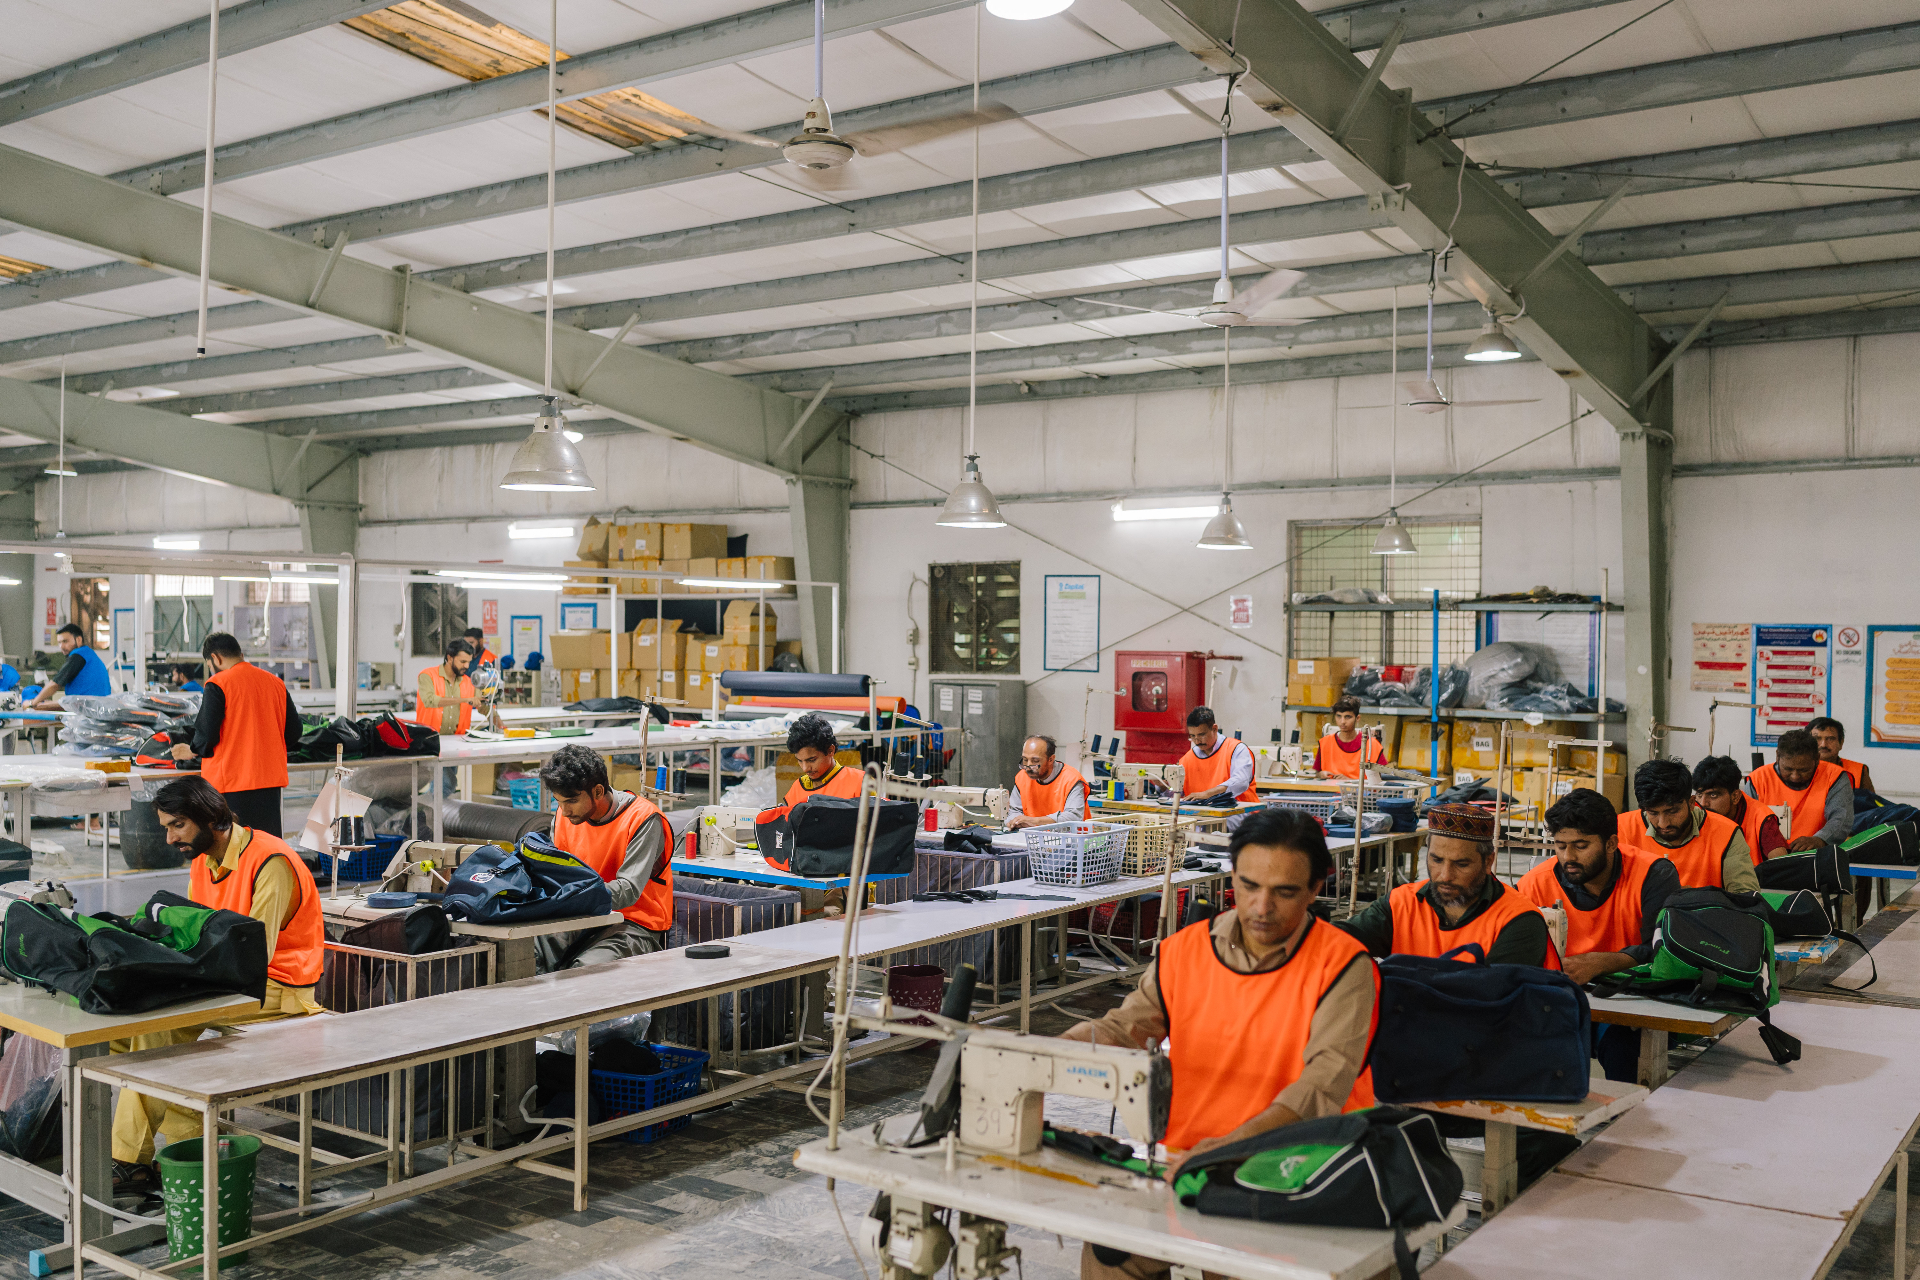
CedarEx Sports Global bridges authentic artisan heritage from Sialkot, Pakistan—the undisputed world capital of hand-stitched and thermo-bonded match balls—with modern European trade infrastructure. Headquartered in Malir Cantonment, Karachi, with production hubs in Sialkot and a European partner office (Penta Flora SRL) in Monterotondo, Italy, we offer an end-to-end OEM manufacturing solution.
Our partner facilities maintain comprehensive international compliance audits, ensuring ethical labor, environmental safety, and uncompromised product quality for international brand partners.
Certified under WRAP, SEDEX/SMETA, and amfori BSCI standards. Zero child labor, fair living wages, and documented worker safety programs across all stitching lines.
ISO 9001:2015 and ISO 14001 certified. Production processes align with WFSGI standards and FIFA Quality Programme lab testing specifications for rebound, sphericity, and air retention.
Seamless international trading under FOB, CFR, CIF, or DDP terms. Direct European invoicing and customs handling through our partner desk in Italy simplifies EU buyer compliance.
Review standardized technical parameters, minimum order quantities, and estimated lead times across our core sporting goods manufacturing categories:
| Product Category | Material / Shell Grade | Inner Bladder & Lining | MOQ (Per Design) | Sample Time | Bulk Lead Time |
|---|---|---|---|---|---|
| Custom OEM Basketballs | Microfiber Composite PU / Vulcanized Rubber | Wound Butyl / Multi-Ply Polyester | 100 Pcs | 7–10 Days | 25–30 Days |
| Hand-Stitched Soccer Balls | 1.4mm PU / High-Gloss TPU | Latex / Butyl Bladder with 4-Ply Canvas | 100 Pcs | 7–10 Days | 25–30 Days |
| Thermo-Bonded Match Balls | Textured Microfiber PU (FIFA Spec) | Syntactic Foam & Laminated Butyl | 150 Pcs | 10–12 Days | 30–35 Days |
| Sublimated Team Jerseys & Kits | 130–180 GSM Mesh / Recycled Polyester | Breathable Moisture-Wicking Finish | 50 Pcs | 7–9 Days | 20–25 Days |
| Boxing & MMA Gear | Genuine Cowhide Leather / Engineered PU | Multi-Layered EVA Foam Mould | 100 Pairs | 10–14 Days | 30–35 Days |
| Carbon Fibre Padel Rackets | 3K / 12K / 18K Carbon Fibre Face | EVA Soft Core (355–375g) | 50 Pcs | 12 Days | 30 Days |
*Note: Air shipping transit typically takes 5–8 days globally. Sea freight averages 18–24 days to Europe and 28–35 days to North American ports.
To eliminate export discrepancies and guarantee absolute adherence to tech pack specifications, CedarEx enforces a rigid four-stage inspection protocol on every production run:
Incoming synthetic leathers, fabric GSM, thread tensile strength, and bladder air retention are lab-tested against client specification sheets prior to cutting.
During assembly, QA inspectors monitor stitch density (stitches per inch), seam alignment, print registration, and adhesive bond strength right on the line.
Randomized sampling evaluates circumference, weight variance, rebound elasticity, and sphericity. Comprehensive photo/video test reports are delivered to the client.
Export carton drop-tests, humidity checks, barcode scanning, container sealing, and issuance of Bills of Lading, COO, and GSP+ documentation.
Clear answers to key operational questions regarding OEM basketball manufacturing, private labeling, logistics, and order execution.