 CedarExSports Global CedarExSports Global
China has become an important sourcing base for quality football equipment, including Hand-Stitched Footballs. Buyers usually inspect more than appearance. They examine panel alignment, stitch tension, bladder retention, rebound, and water resistance.
FIFA’s Quality Programme for Footballs evaluates circumference, sphericity, rebound, weight, pressure loss, and water absorption. These tests show why craftsmanship remains commercially important. Grand View Research and Statista also identify football equipment as a substantial global sports category, supported by club purchases, schools, academies, and recreational demand. However, market reports often group machine-stitched and hand-stitched products together. That limitation deserves attention.
Dr. Andy Harland, a football aerodynamics researcher at Loughborough University, has said, “A football is a very complex object.” His observation applies directly to hand stitching. A skilled operator can control seam depth around each panel, but small variations may still occur. No workshop is flawless. That is why responsible Chinese manufacturers combine experienced stitching teams with measurable inspections and documented production controls.
For global buyers, the strongest supplier is not simply the lowest-cost factory. It is a manufacturer that can explain materials, thread specifications, bladder options, sampling procedures, and quality records clearly. A well-made Hand-Stitched Football should feel balanced in the hand, hold pressure overnight, and maintain a stable flight after repeated use. Those details are easy to overlook. They should not be. This guide examines how Chinese manufacturers build, test, and supply Hand-Stitched Footballs for international buyers seeking dependable performance and transparent cooperation.
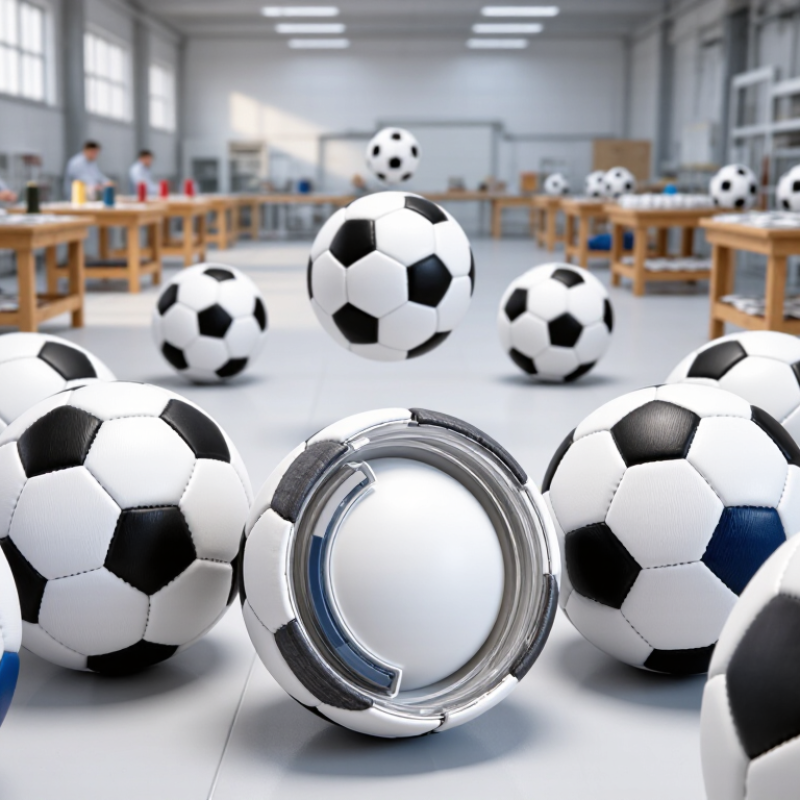
For global buyers, hand-stitched footballs must meet measurable FIFA Size 5 requirements. The IFAB Laws of the Game 2024/25 specify a circumference of 68–70 cm and a weight of 410–450 g. These figures guide material selection, panel cutting, stitching tension, and final inspection.
A reliable production process begins with calibrated panels. Skilled workers align each seam by hand, keeping the ball round rather than merely attractive. Inspectors then measure circumference at several points and weigh every approved sample. FIFA’s Quality Programme for Footballs also evaluates shape retention, rebound consistency, water absorption, and pressure loss. Small failures can affect passing accuracy.
Hand stitching leaves useful evidence. Thread tension should look even, with no loose loops or crushed panel edges. The surface should feel firm but not harsh under the thumb. Inflation tests matter too. A ball that reaches the correct weight may still lose pressure too quickly. That is easy to overlook.
The standards are clear.
However, measurements alone do not describe match performance. Factory records, sample testing, and traceable inspections provide stronger evidence for importers. Buyers should request current test results and production samples before placing large orders. European and Asian weather conditions can differ, so storage testing deserves attention. A careful manufacturer accepts that no batch is perfect, and improves its process when inspection data exposes weakness.
| Specification | Standard / Typical Requirement | Why It Matters to Global Buyers |
|---|---|---|
| Ball Size | Size 5 | The standard full-size football category for adult matches and most competitions for players aged approximately 13 and above. |
| Circumference | 68–70 cm | Matches the size range specified in the IFAB Laws of the Game for a standard match ball. |
| Weight | 410–450 g at the start of the match | Provides a recognized full-size match-ball weight range for international and domestic football markets. |
| Internal Pressure | 0.6–1.1 atmosphere (600–1,100 g/cm²) | Supports consistent rebound, flight, and handling when inflated and tested within the official playing range. |
| Construction Method | Hand-stitched panel construction | Hand stitching can provide strong seam reinforcement and is suitable for training, match, promotional, and institutional supply programs. |
| Outer Cover | Commonly laminated synthetic leather, such as PU or PVC, subject to the product specification | Synthetic covers offer configurable touch, abrasion resistance, appearance, and cost for different market segments. |
| Bladder Options | Butyl or latex bladder, depending on the selected model | Butyl generally offers stronger air retention, while latex is valued for a softer feel and responsive play characteristics. |
| Panel Configuration | According to the approved product pattern; panel count and geometry may vary | Panel design influences roundness, aerodynamics, visual appearance, and manufacturing cost. |
| Shape and Roundness | Spherical form with consistent panel alignment and seam tension | A consistent shape helps improve predictable flight, ball control, and repeatable production quality. |
| Intended Applications | Club training, school programs, recreational play, retail, events, and match use subject to certification | Allows importers and distributors to select specifications based on performance, budget, and market positioning. |
| Pre-Shipment Checks | Visual inspection, circumference measurement, weight measurement, inflation test, valve check, and seam inspection | Documented inspections help reduce dimensional variation, leakage issues, cosmetic defects, and shipment disputes. |
Note: The circumference, weight, and pressure ranges above are based on the IFAB Laws of the Game requirements for a standard match ball. Official competition approval or certification requires separate testing against the applicable governing-body requirements.
PU usually feels softer and grips better in cool, dry sessions. PVC resists abrasion and costs less. Cold weather can make PVC feel firm. Our first sample may not be right.
Butyl bladders hold air reliably and suit regular training. Latex bladders provide livelier rebound but need more frequent inflation. The better choice depends on maintenance expectations.
A 0.6 mm layer keeps the ball light and flexible. A 0.8 mm layer often improves roundness and scuff resistance. A 1.0 mm layer adds durability but may reduce softness.
Inspect panel bonding, stitch spacing, bladder centering, circumference, weight, rebound, and pressure stability. Small defects matter. A polished surface can hide uneven lamination.
Test samples under the target climate, playing surface, and age group. Recheck them after cold storage, wet handling, and repeated impacts. One test is not enough.
Ask for recent capacity figures, worker numbers, equipment details, and production schedules. Review cutting, stitching, lining, bladder, and inspection areas. Photographs alone prove little.
Request certificate numbers, issuing bodies, product scope, and expiry dates. Check chemical safety, durability, and colorfastness requirements. A certificate cannot prove every batch is consistent. Retained samples help.
Confirm MOQ for each color, size, and panel design. Separate sample approval, material preparation, stitching, inspection, and export booking. Add buffer days. Printed panels can arrive late.
Confirm trade terms, packaging, shipping documents, payment stages, and customs responsibilities. Request carton markings and loading photographs. Risks should be explained openly, even when inconvenient.
Hand-Stitched Footballs are valued by global buyers for their durability, consistent shape, and reliable match performance. A standard FIFA Size 5 ball generally measures 68–70 cm in circumference and weighs 410–450 g. Careful panel cutting and precise hand-stitching help maintain roundness, balance, and stable flight. Manufacturers may select PU or PVC covers according to the intended use, while suitable bladders and 0.6–1.0 mm lamination can improve touch, strength, and resistance to wear.
For professional supply, quality testing should cover weight, roundness, rebound, water absorption, and pressure loss. Buyers should also evaluate a factory’s production capacity, quality certifications, minimum order quantity, lead time, and export terms. A dependable supplier should provide consistent workmanship, transparent specifications, efficient production planning, and suitable packaging for international shipment. These factors help buyers choose Hand-Stitched Footballs that meet performance expectations and support stable, long-term purchasing needs.